default alt
default alt
default alt
default alt
default alt
default alt
Carbon dioxide recovery system for dry ice production
Recovery of carbon dioxide lost during dry ice production During the production of dry ice, a large portion of the carbon dioxide feeding a dry ice machine is released as a gas instead of being converted into dry ice. This gas, often known as a CO2 return gas, can be recovered, compressed, re-liquefied and returned to a liquid CO2 storage tank for reuse. YTC's CO2 recovery systems for dry snow are specifically designed to recover that CO2 that would otherwise be wasted and put back into the production cycle. The system helps dry ice manufacturers improve their CO2 utilization rate, reduce raw material consumption, reduce production costs, and reduce CO2 emissions. Key advantages • Carbon dioxide utilization rate: Raising the overall utilization rate to 2%, by 95 ‑ 90%, to up to 45 ‑ 40 CO2 from approximately operating conditions and system configuration • Reduce CO2 consumption: Restore and reuse carbon dioxide that would have been released to the atmosphere • Reduce operating costs: Reduce reliance on external supply of CO2 • Reduce emissions: Reduce loss of carbon dioxide during dry ice production • Automated operation: Control system by PLC to ensure stable and reliable operation • Compact design: designed for efficient integration with existing dry ice production facilities • Easy installation: Pre-plugged and wire configuration is available to simplify the installation process
Carbon dioxide recovery capacity:
Customized according to dry ice production capacity
Carbon dioxide purity:
up to 98%
Carbon dioxide utilization rate:
up to 95%
Technology:
CO2 return gas recovery, compression and re-liquefaction
Output:
Liquid carbon dioxide recovered
Dry Ice Production CO₂ Recovery System

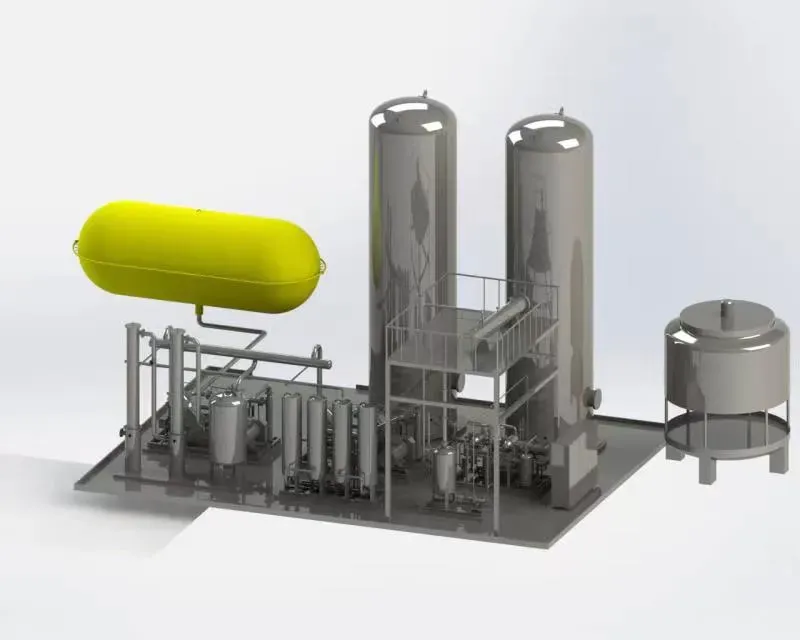
How the Dry Ice CO₂ Recovery System Works

The recovery system captures CO₂ released during dry ice production and converts it back into liquid CO₂ for reuse.

1. CO₂ Revert Gas Collection

During the production of dry ice blocks, pellets, or other forms, part of the supplied CO₂ is released as gas. This CO₂ revert gas is collected instead of being discharged into the atmosphere.

2. CO₂ Buffer System

A dedicated CO₂ buffer balloon provides temporary storage and stabilizes the pressure and flow of the recovered gas.

The buffer system is designed using suitable food-contact-compatible materials and provides a stable gas supply to the recovery compressor. Depending on local operating conditions, a gas reheating system can also be incorporated.

3. CO₂ Compression

The recovered CO₂ is compressed using a water-cooled, dry-running, oil-free two-stage CO₂ piston compressor.

Separate cooling between compression stages helps maintain stable operating conditions. The recovered gas can be compressed to approximately 18–20 barg, depending on the system design.

4. CO₂ Reliquefaction

The compressed CO₂ enters the refrigeration and liquefaction system, where it is cooled and converted back into liquid CO₂.

The reliquefied CO₂ is then returned to the liquid CO₂ storage tank for reuse in dry ice production.

5. Automatic Control

A centralized PLC control system automatically manages the recovery process, including compressor operation, refrigeration, pressure control, monitoring, and system protection.

The automated design allows the recovery system to operate continuously with the dry ice production line.

Why Recover CO₂ from Dry Ice Production?

  • Improve CO₂ Utilization

Dry ice production naturally generates CO₂ losses. Recovering this gas allows more of the purchased CO₂ to be utilized in the production cycle.

  • Reduce CO₂ Consumption

Recovered CO₂ is reliquefied and returned to the storage tank, reducing the amount of fresh liquid CO₂ required for the same dry ice output.

  • Reduce Production Costs

By recovering and reusing otherwise wasted CO₂, dry ice producers can reduce raw material consumption and improve overall production economics.

  • Reduce CO₂ Emissions

The system minimizes CO₂ released during dry ice production, supporting more efficient resource utilization and improved environmental performance.

  • Improve Production Efficiency

Continuous recovery and reuse of CO₂ helps maximize the output obtained from each unit of CO₂ supplied to the dry ice production line.

YTC Dry Ice CO₂ Recovery Solution

YTC provides integrated CO₂ revert gas recovery, compression, reliquefaction, and control systems for dry ice production facilities.

The recovery system can be integrated with existing dry ice pelletizers, block machines, and other CO₂-based dry ice production equipment. System capacity and configuration are selected according to dry ice production capacity, CO₂ consumption, operating conditions, and site requirements.

With 20+ years of experience in CO₂ treatment and recovery and 200+ CO₂ projects completed worldwide, YTC provides engineering, equipment manufacturing, installation, commissioning, and technical support for complete CO₂ recovery solutions.

By recovering CO₂ that would otherwise be lost during dry ice production, YTC helps producers recover more, consume less, and improve the overall economics of dry ice manufacturing.

Related Products
default alt
Electronic-grade CO₂ recovery system
Ultra-High-Purity CO₂ Recovery for Semiconductor Manufacturing Semiconductor manufacturing requires CO₂ with exceptionally high purity and tightly controlled trace impurities. Moisture, oxygen, hydrocarbons, particles, and other contaminants can affect sensitive processes and product quality. YTC Electronic-Grade CO₂ Recovery Systems are designed to recover, purify, compress, liquefy, and continuously supply high-purity CO₂ for demanding semiconductor applications. Building on YTC’s established CO₂ recovery and purification technology, the system incorporates advanced purification and monitoring stages to control critical impurities at sub-ppm levels.
default alt
Liquid CO₂ Storage Tank
Reliable Bulk Storage for High-Purity Liquid CO₂ The YTC Liquid CO₂ Storage Tank is engineered for the safe and reliable bulk storage of liquefied carbon dioxide (LCO₂) after purification and liquefaction. As a critical part of a complete CO₂ recovery and distribution system, the storage tank provides a controlled buffer between continuous CO₂ production and downstream consumption, tanker loading, dry ice production, or other liquid CO₂ applications. YTC engineers each storage system according to the customer's liquid CO₂ production capacity, required storage volume, operating pressure, delivery frequency, reserve requirements, site conditions, and applicable pressure-vessel standards. The storage system can integrate the pressure vessel, thermal insulation, filling and withdrawal piping, valves, pressure and liquid-level instrumentation, safety devices, and automatic controls into a complete liquid CO₂ storage solution.
default alt
One Stop CO2 RECOVERY SYSTEM Solution For Your Project
YTC company owned over 100+ staffs, including experts, senior engineers, and advanced technologists. This diverse team with innovative thinking can provide you with comprehensive project solutions all in one place.
Contact Us