The Core Pressure-Raising Stage
Recovered CO₂ normally enters the recovery plant at relatively low pressure. Before it can be deeply dried, purified and liquefied, its pressure must be increased to an appropriate operating level.
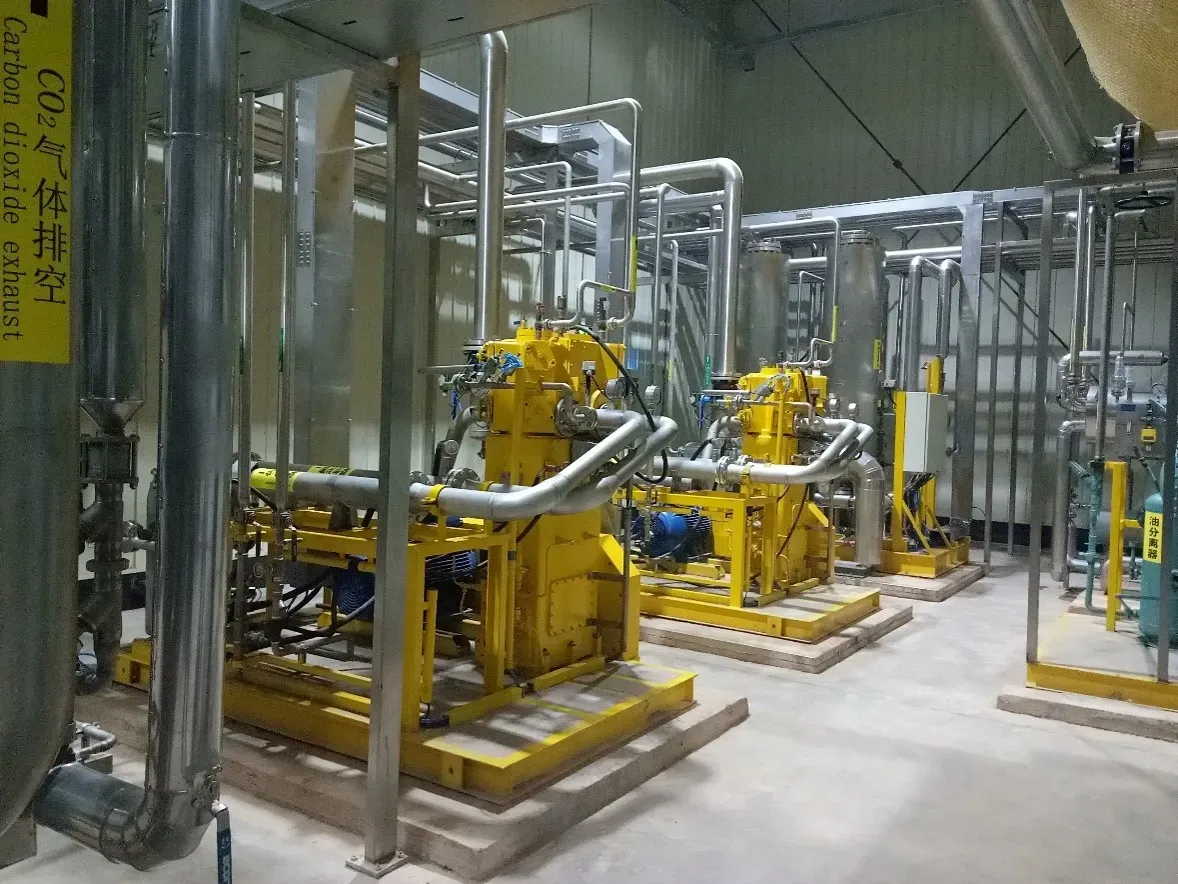
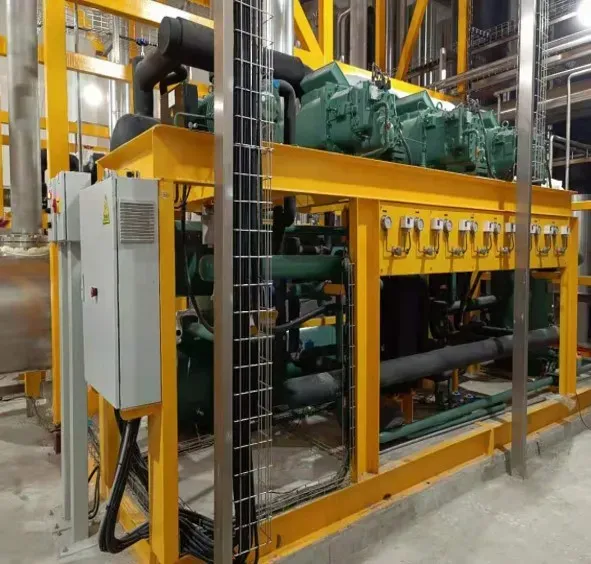
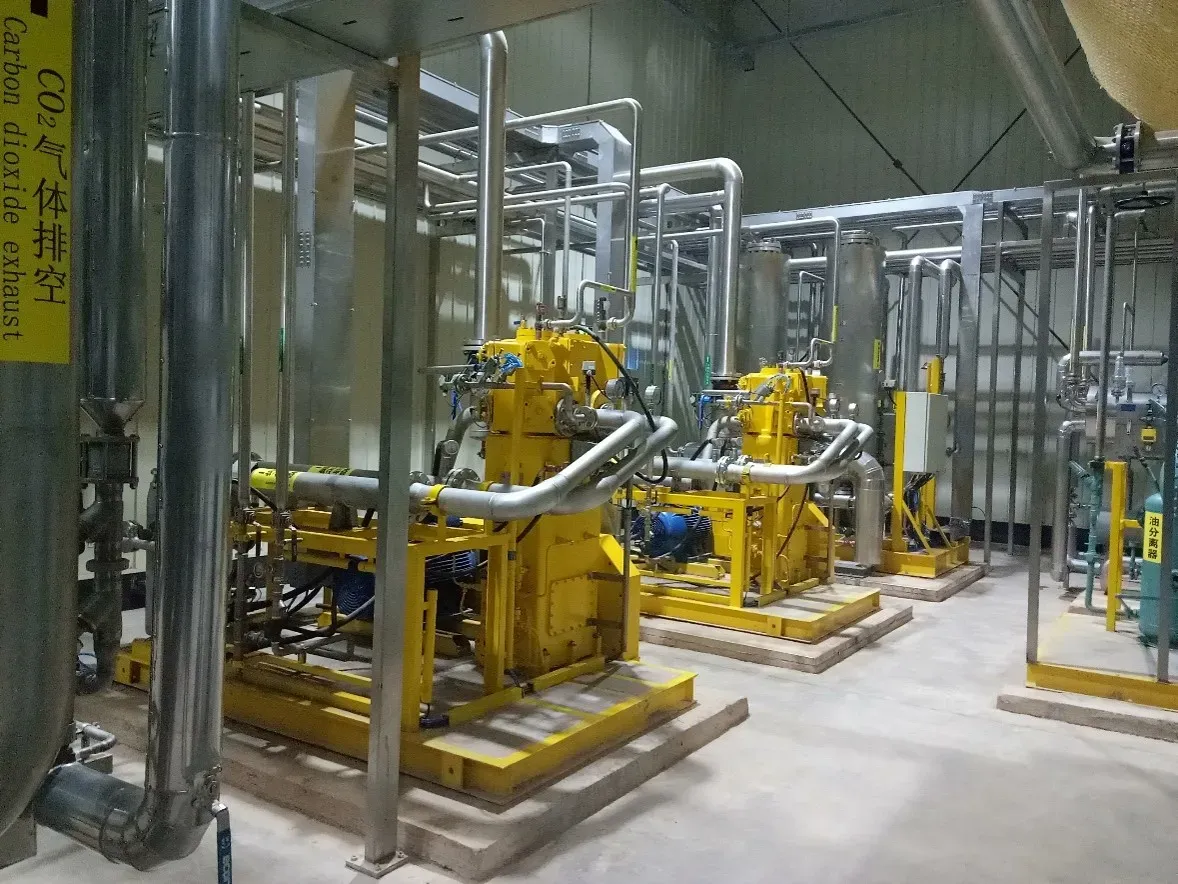
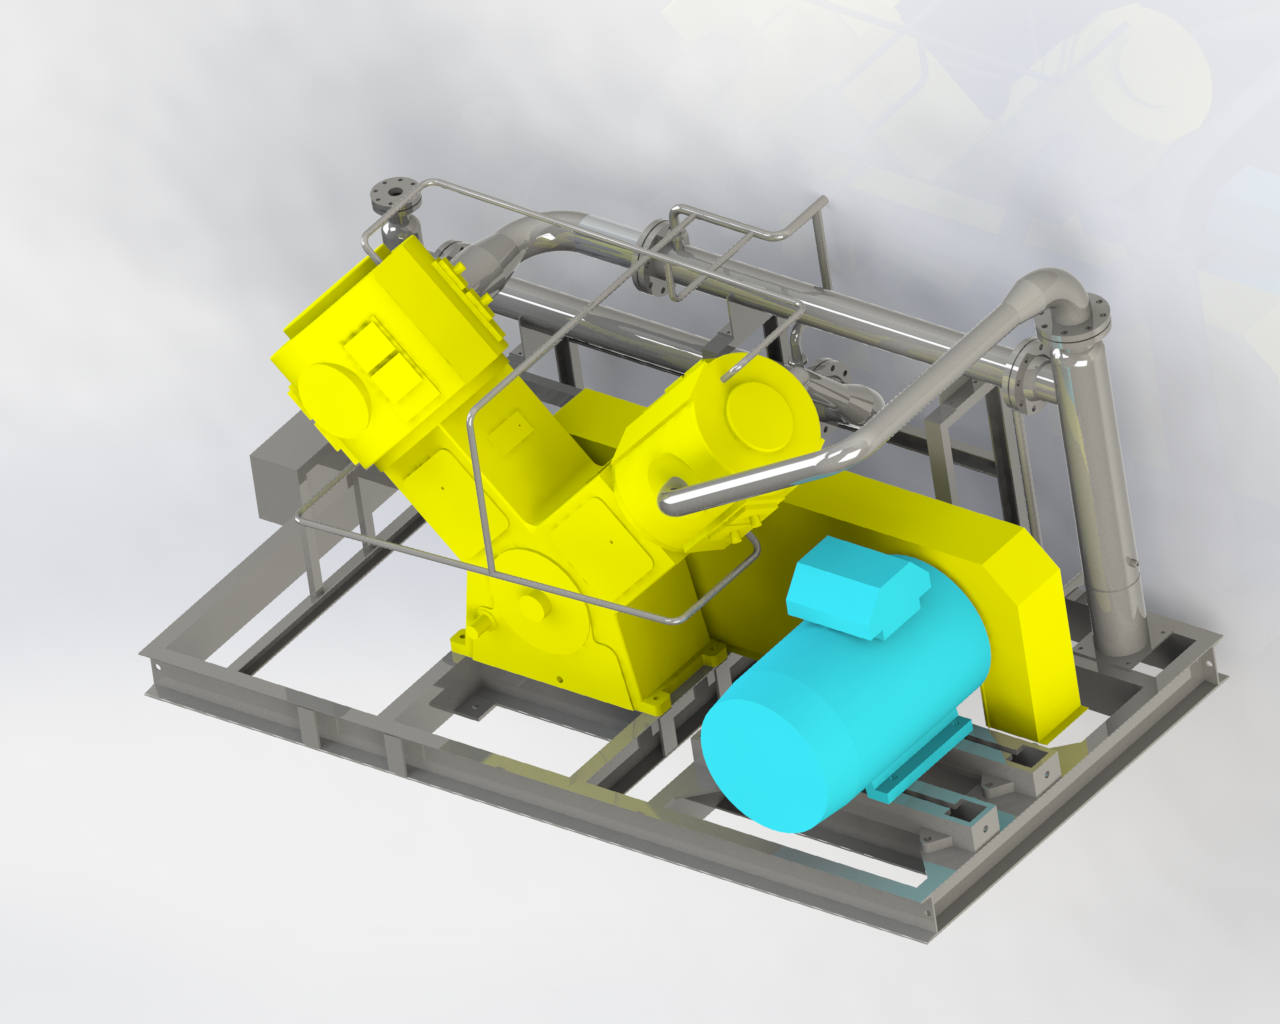
The CO₂ Compressor Unit performs this essential function.
Compression is not simply a mechanical operation. It influences the temperature, phase behavior, moisture content and energy consumption of the entire downstream process.
For this reason, YTC treats the compressor as an integrated process unit within the CO₂ recovery system.
Compression According to Process Requirements
The required compression ratio depends on the source gas and final liquefaction conditions.
Key design parameters include:
- CO₂ inlet pressure
- CO₂ outlet pressure
- Gas flow rate
- Gas temperature
- CO₂ concentration
- Moisture content
- Required liquid CO₂ production
- Operating hours
- Downstream liquefaction conditions
The compressor configuration is selected according to these parameters rather than using a single standard configuration for all projects.
Multi-Stage Compression
Where a high pressure ratio is required, multi-stage compression can be used.
The gas temperature increases during compression. Interstage cooling reduces the gas temperature before it enters the next compression stage.
Condensed moisture can then be separated between stages.
This arrangement improves compression efficiency and helps prevent excessive moisture from being carried into the downstream adsorption dryer.
Upstream Gas Conditioning
Compressor reliability begins before the compressor itself.
Raw fermentation CO₂ can contain foam and entrained liquid. The Defoaming Washing System therefore provides an important protective function.
By reducing free liquid and foam before compression, the upstream pretreatment system helps maintain more stable compressor operating conditions.
This illustrates an important principle of YTC's system design: the compressor is engineered together with the gas pretreatment system rather than treated as an isolated machine.
Interstage Cooling and Condensate Removal
Cooling after compression can cause water and other condensable components to separate from the gas.
The process can therefore incorporate interstage coolers and gas-liquid separators.
Removing condensate at this stage reduces the moisture burden on the adsorption dryer.
It also improves the overall efficiency of the purification chain.
Compressor Efficiency
Compression is one of the major energy-consuming operations in a CO₂ recovery plant.
The selection of compressor capacity, number of stages, compression ratio and cooling configuration therefore has a direct influence on the operating cost of the plant.
YTC's engineering approach considers compressor performance together with the complete process flow, including the subsequent drying and liquefaction requirements.
The objective is to provide the required pressure while maintaining stable operation and reasonable energy consumption.
Automatic Control and Protection
The compressor unit can be integrated with the central DCS.
Pressure and temperature sensors provide continuous information about compressor operating conditions.
The control system can manage startup and shutdown sequences and provide alarms for abnormal conditions.
Depending on the project configuration, protective functions can include high discharge pressure, abnormal temperature, low suction pressure and other critical conditions.
Adaptation to Different Feedstocks
The compressor section may operate under significantly different conditions depending on the CO₂ source.
Fermentation CO₂ typically requires careful control of moisture and organic contaminants.
Flue-gas recovery may require more extensive upstream purification.
Natural-gas and process-gas applications may require attention to hydrocarbon content and other trace components.
The compressor must therefore be selected after understanding the actual gas composition.
Connection to Downstream Purification
After compression, the CO₂ proceeds to the adsorption and drying section.
Higher pressure provides suitable conditions for subsequent purification and liquefaction.
The compressor therefore represents the transition between raw-gas recovery and high-pressure CO₂ processing.
YTC Integrated Manufacturing and Engineering
YTC's official website identifies its business as covering CO₂ gas treatment and recovery equipment manufacturing and engineering, with independent design, manufacturing, installation and commissioning capabilities. Its published project range extends from approximately 80 kg/h to 20,000 kg/h.
This integrated capability allows the compressor unit to be matched to the complete plant rather than designed independently.
Reliable Compression for Liquid CO₂ Production
A reliable compressor provides the pressure foundation for the downstream process.
Combined with effective washing, drying, purification and refrigeration, the CO₂ Compressor Unit enables recovered gas to move efficiently toward high-purity liquid CO₂ production.