

How CO₂ Recovery Works in an Ethanol Plant
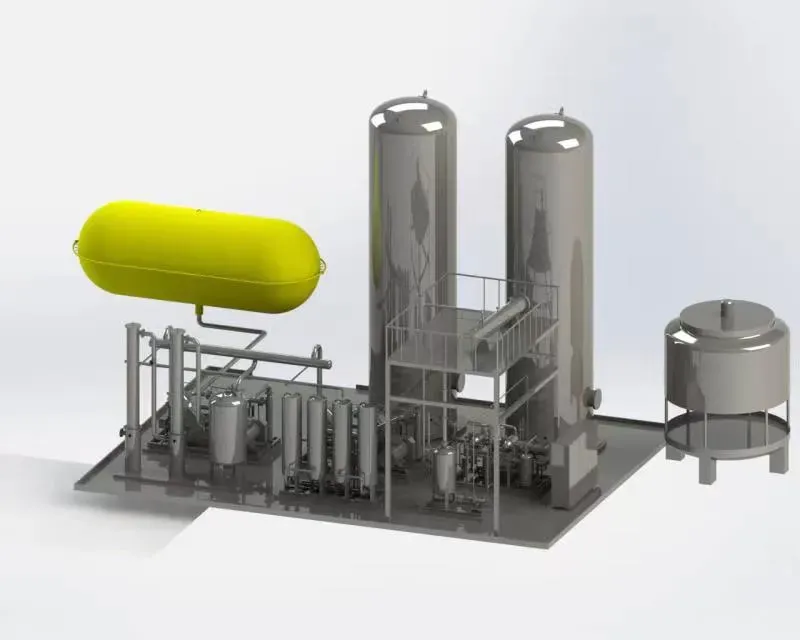
The CO₂ recovery process begins with the fermentation section of the ethanol plant, where microorganisms convert sugars into ethanol and CO₂. The fermentation gas is continuously collected and transferred to the CO₂ recovery system.
1. CO₂ Collection
CO₂ generated during ethanol fermentation is collected through a dedicated gas collection system and continuously supplied to the recovery plant.
2. Gas Washing and Defoaming
The raw fermentation gas may contain ethanol vapor, water droplets, foam, and other entrained impurities. A washing and defoaming system removes these contaminants and protects downstream equipment.
3. CO₂ Compression
The pre-treated CO₂ gas is compressed to the required operating pressure, reducing its volume and preparing it for subsequent purification and liquefaction.
4. Purification and Drying
Advanced purification and adsorption technologies remove moisture and trace impurities from the compressed CO₂. Effective drying is essential for stable downstream liquefaction and high-quality liquid CO₂ production.
5. CO₂ Liquefaction
The purified CO₂ is cooled and liquefied through the refrigeration and liquefaction system. During this stage, non-condensable gases such as O₂ and N₂ are separated from the liquid CO₂.
6. Final Purification
The liquid CO₂ passes through the final purification and stripping process to further reduce residual impurities, particularly oxygen. The system can produce high-purity CO₂ up to 99.998%, depending on the feed gas composition and process configuration.
7. Liquid CO₂ Storage
The purified liquid CO₂ is transferred to insulated storage tanks for continuous plant operation. The recovered CO₂ can then be used internally, supplied to downstream industries, or loaded for commercial distribution.
Why Recover CO₂ from Ethanol Fermentation?
- Reduce CO₂ Purchasing Costs
Recovering CO₂ directly from the ethanol fermentation process can significantly reduce dependence on externally purchased CO₂ and provide greater control over long-term gas supply costs.
- Turn a By-Product into a Valuable Product
CO₂ is a natural by-product of ethanol fermentation. With appropriate recovery and purification, this gas can be converted into high-purity liquid CO₂ suitable for a range of downstream applications.
- Improve Resource Utilization
On-site CO₂ recovery allows ethanol plants to make better use of existing process resources while reducing unnecessary CO₂ emissions to the atmosphere.
- Support Continuous Production
An integrated recovery, liquefaction, and storage system enables continuous CO₂ production while providing a buffer for downstream consumption, tanker loading, or seasonal demand.
- Automated and Reliable Operation
YTC systems incorporate automated PLC/DCS control, online monitoring, and integrated process control to simplify operation and maintain stable system performance with limited manual intervention.
- CO₂ Applications
Recovered liquid CO₂ from ethanol fermentation can be supplied for a variety of applications, subject to the required product specifications and applicable regulations, including:
• Beverage carbonation
• Food processing and food preservation
• Dry ice production
• Industrial gas applications
• Greenhouse CO₂ enrichment
• Commercial liquid CO₂ supply
YTC Ethanol CO₂ Recovery Solution
YTC provides complete CO₂ recovery and purification solutions for ethanol and alcohol fermentation plants, from process design and equipment manufacturing to installation, commissioning, and technical support.
With 20+ years of experience in CO₂ treatment and recovery and 200+ CO₂ recovery projects completed worldwide, YTC designs each system according to the customer’s fermentation process, CO₂ generation rate, feed gas composition, site conditions, required product quality, and downstream application.
The result is a reliable and economical solution that enables ethanol producers to recover more CO₂, reduce operating costs, improve resource efficiency, and create additional value from fermentation by-products.